Turning and facing
Parallel and stepped diameters, shoulders and faces turned to size with the finish needed for a seal or bearing to run on.
Unit 8 Leaside, Aycliffe Business Park, Newton Aycliffe, DL5 6HX
Monday to Friday, 8:00am – 4:30pm
Manual Turning & Machining
Turning, boring, facing and thread cutting on manual lathes — the fastest route to a one-off shaft, bush, rod or flange.
For round work — shafts, rods, bushes, spacers, flanges and cylinder components — a skilled hand on a manual lathe is still the quickest and most economical route to a finished part. There is no programming time and no fixturing to design, so a job can go from bench to blueprint to finished component inside a single visit. On breakdown work, that difference is measured in machine downtime.
Manual turning is also the right tool for parts that are not quite what the drawing says any more. Worn housings, stretched threads and repaired bores rarely sit on nominal dimensions, and cutting to suit the actual measured part is something an experienced turner does naturally.
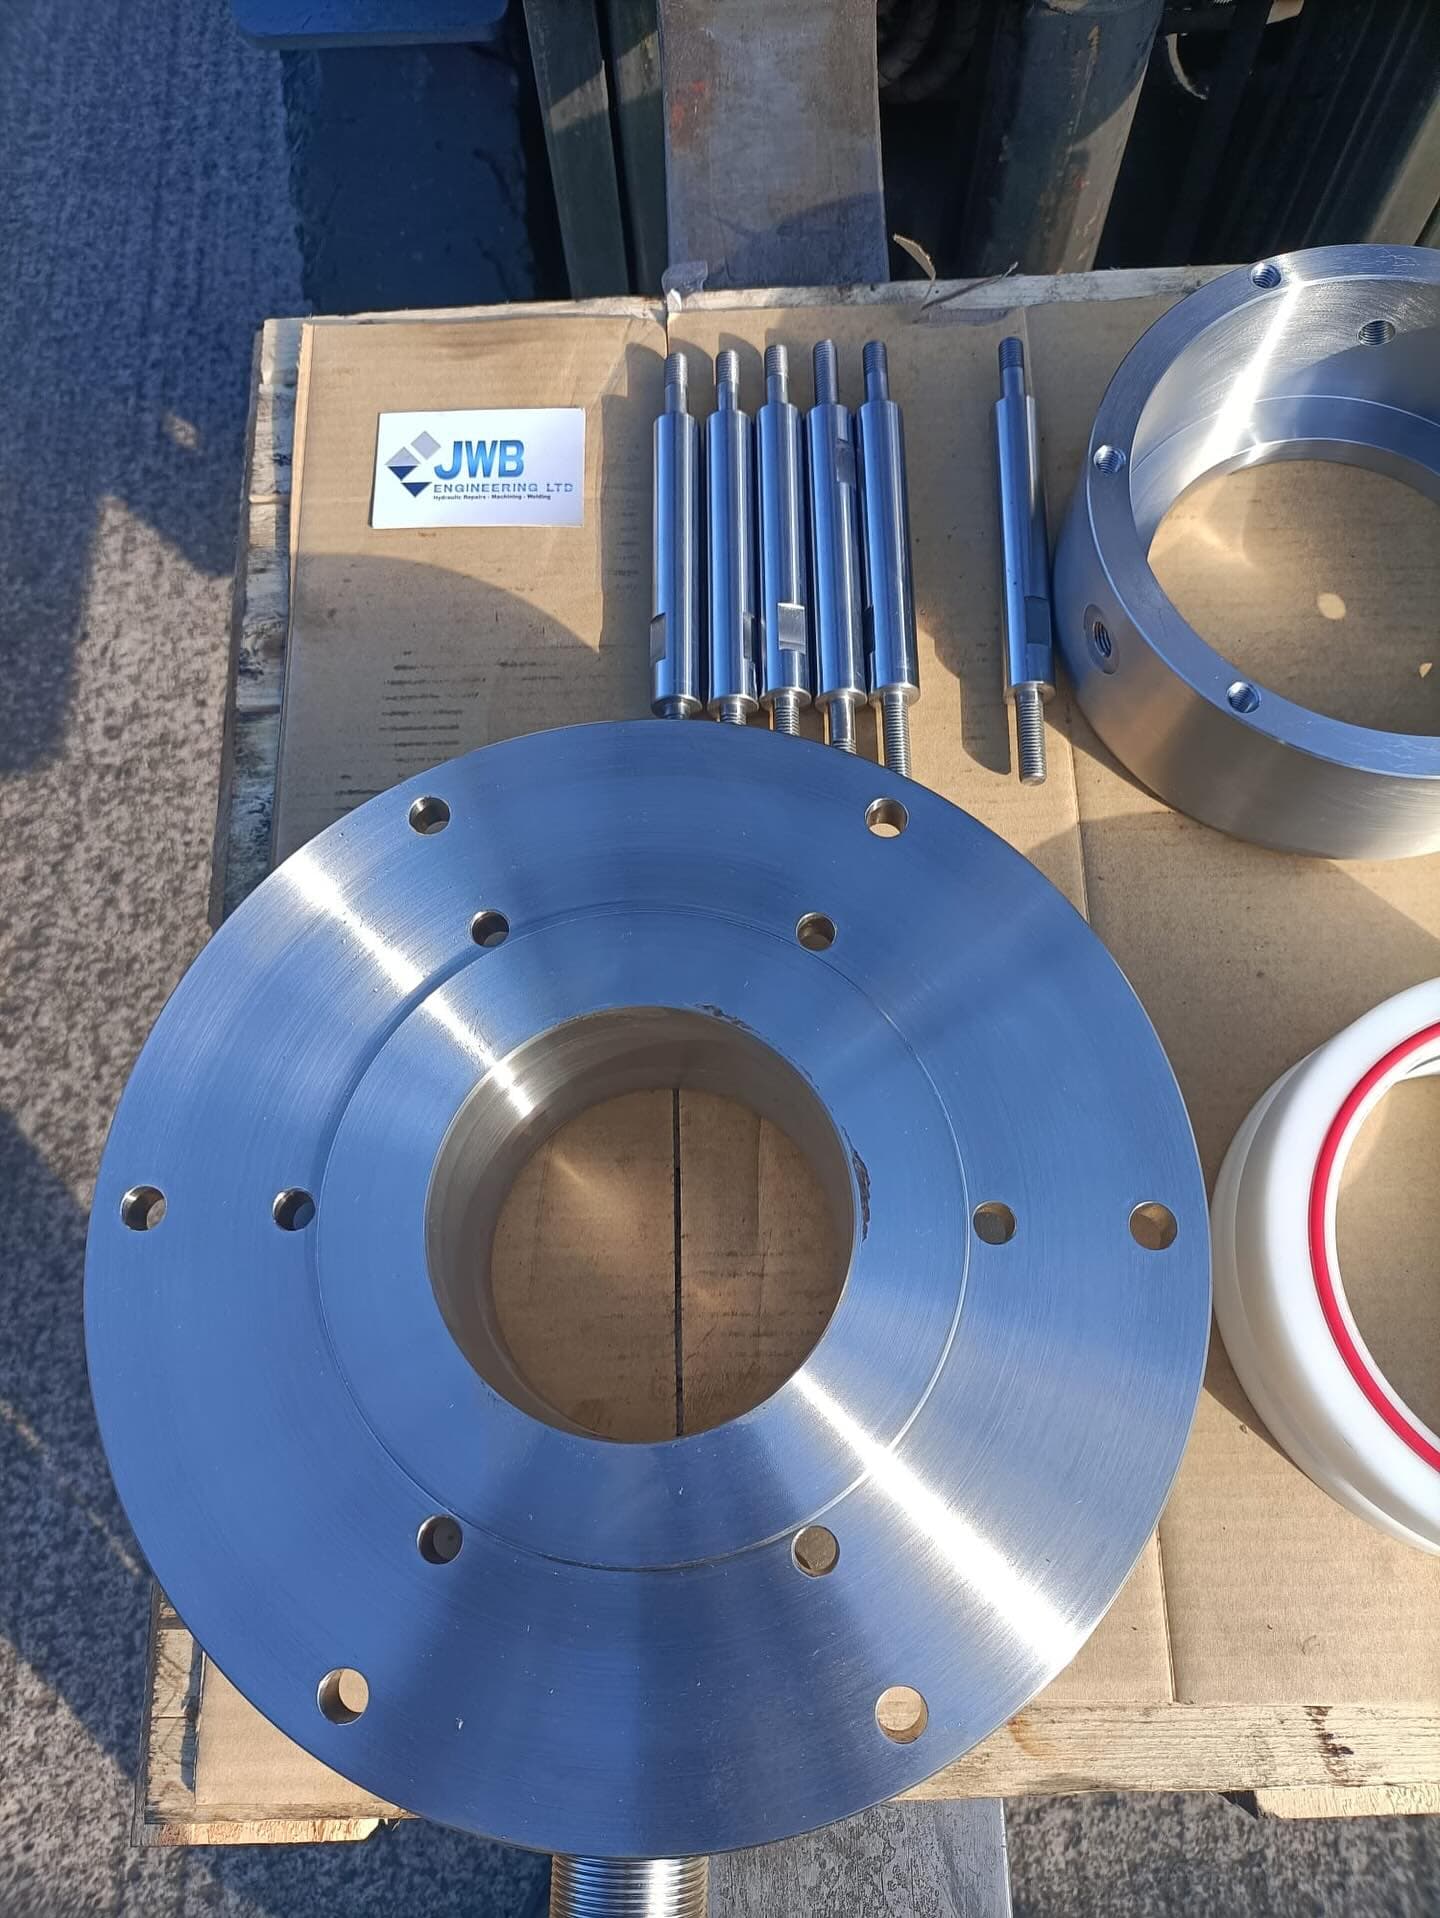
Describe the part or the fault and we will tell you honestly whether it is worth repairing. If it is not, we will say so.
Call 01325 522430Send an enquiryThe detail of a job varies, but these are the operations that make up most manual turning & machining work we take on.
Parallel and stepped diameters, shoulders and faces turned to size with the finish needed for a seal or bearing to run on.
Worn bores opened up and sleeved back to original size, restoring a housing rather than replacing the whole assembly.
Internal and external threads cut on the lathe, including non-standard and imperial pitches, plus recovery of damaged threads on existing components.
Replacement shafts, hydraulic rods, pivot pins and studs made from stock to match a sample or drawing.
Bronze, steel and engineering plastic bushes, spacers and wear sleeves turned to fit the housing they are going into.
Components for machinery that is long out of production, made from the worn original where no drawing survives.
Tell us what you have and what has gone wrong. Include dimensions if you have them, and say if the machine is currently out of service.
Most jobs draw on more than one of these. Because everything happens in the same workshop, a part can be welded, machined and rebuilt without leaving the building.
Strip-down, assessment and rebuild of hydraulic cylinders and rams, from single-acting tipping rams to bespoke multi-port cylinders.
Read moreCNC milling for housings, manifold blocks, flanges and prismatic parts, worked to drawing or reverse-engineered from a sample.
Read moreTIG and MIG welding on stainless and mild steel, from hydraulic pipework and manifold assemblies to structural repair and bespoke fabrication.
Read moreWorn and damaged components restored to serviceable condition, typically at a fraction of the cost of buying new.
Read moreMost enquiries start with a description of a problem rather than a specification. Tell us what the machine is doing and we will work out the rest.
Get in touch