Strip-down and condition report
Every cylinder is dismantled, cleaned and measured before we quote the repair. You get a clear account of what has actually failed, what is reusable, and what needs replacing or remaking.
Unit 8 Leaside, Aycliffe Business Park, Newton Aycliffe, DL5 6HX
Monday to Friday, 8:00am – 4:30pm
Hydraulic Cylinder Repairs
Strip-down, assessment and rebuild of hydraulic cylinders and rams, from single-acting tipping rams to bespoke multi-port cylinders.
A hydraulic cylinder rarely fails without warning. Weeping seals, a scored rod, a drifting ram that will not hold load — these are all signs that the cylinder needs attention before it strands the machine it is fitted to. We strip, assess and rebuild hydraulic cylinders and rams at our workshop on Aycliffe Business Park, and we machine the replacement parts ourselves rather than waiting on a supplier.
Because we have the lathe and mill in the same building as the bench, we can make an undersized gland, an oversized piston or a one-off rod end to suit the cylinder in front of us. That matters most on older or obsolete equipment where the seal kit is no longer catalogued and a replacement cylinder either does not exist or costs many times the price of a repair.
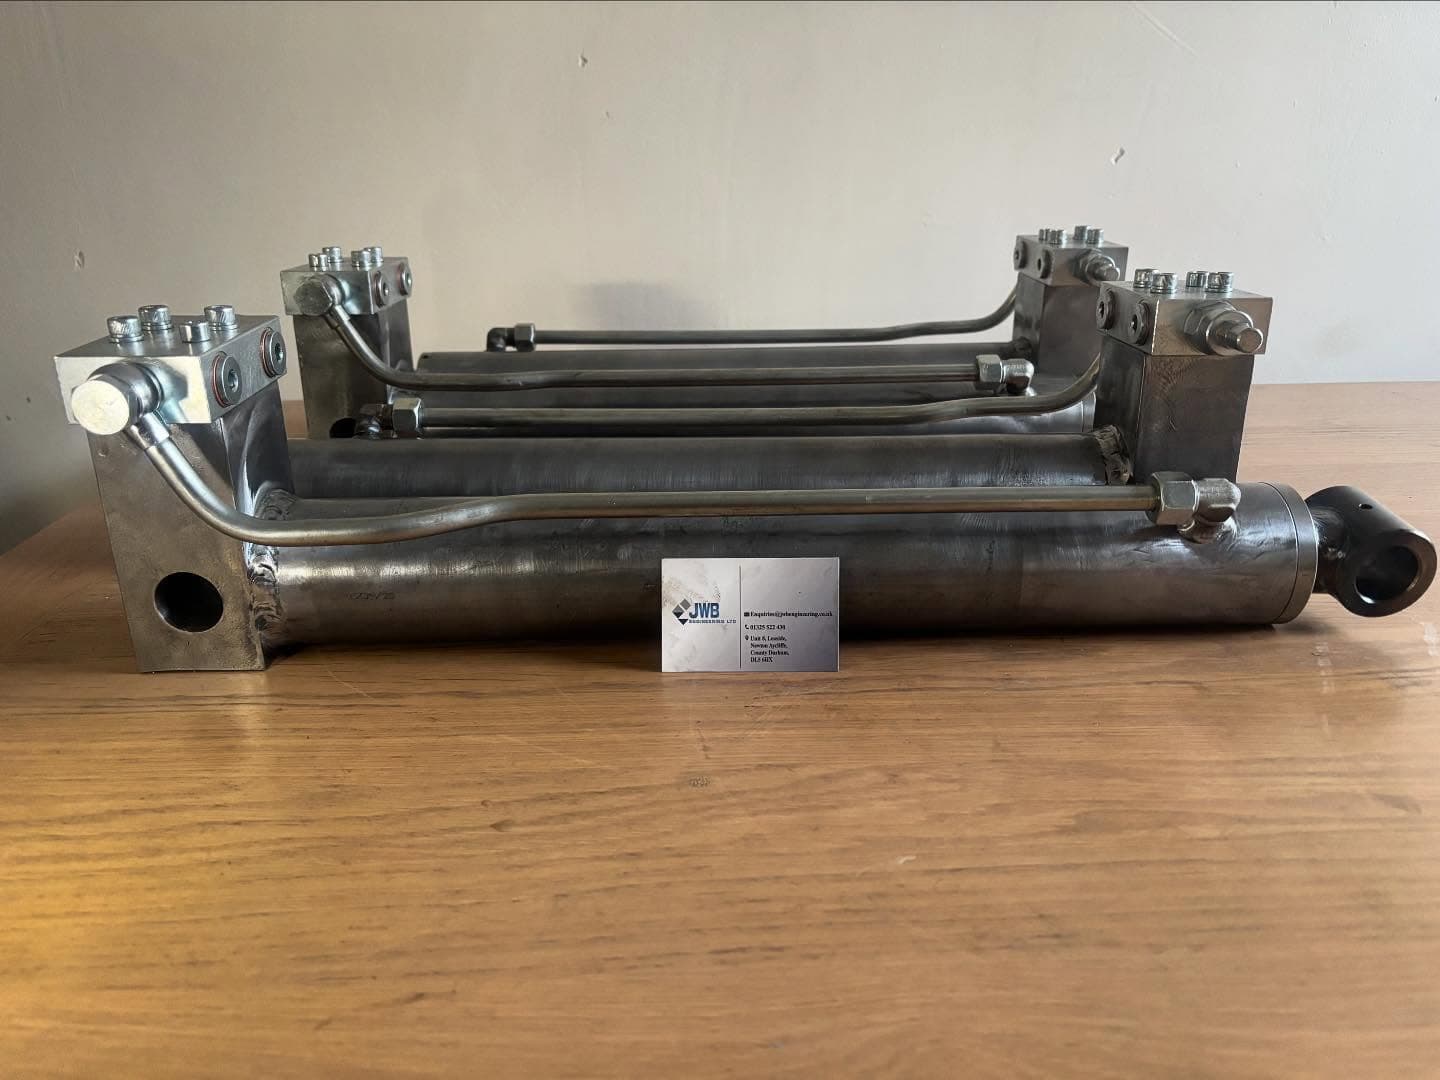
Describe the part or the fault and we will tell you honestly whether it is worth repairing. If it is not, we will say so.
Call 01325 522430Send an enquiryThe detail of a job varies, but these are the operations that make up most hydraulic cylinder repairs work we take on.
Every cylinder is dismantled, cleaned and measured before we quote the repair. You get a clear account of what has actually failed, what is reusable, and what needs replacing or remaking.
Seal kits sourced to specification, or measured and matched from the old seals where the kit is obsolete. We also machine nylon and PTFE seal carriers and wear rings in-house.
Honing to restore bore finish and remove light scoring, plus barrel replacement where wear or corrosion has gone beyond a serviceable limit.
New rods turned and finished to size, thread repair and re-cutting, and replacement rod eyes and spherical bearing housings fitted and welded where required.
Where repair is not viable we build a replacement to match the original mounting centres, bore, stroke and port positions, including welded manifold blocks and formed steel pipework.
Orbital and gear motor strip-down, inspection and refurbishment, returned cleaned, resealed and tested for fit.
Tell us what you have and what has gone wrong. Include dimensions if you have them, and say if the machine is currently out of service.
Most jobs draw on more than one of these. Because everything happens in the same workshop, a part can be welded, machined and rebuilt without leaving the building.
CNC milling for housings, manifold blocks, flanges and prismatic parts, worked to drawing or reverse-engineered from a sample.
Read moreTurning, boring, facing and thread cutting on manual lathes — the fastest route to a one-off shaft, bush, rod or flange.
Read moreTIG and MIG welding on stainless and mild steel, from hydraulic pipework and manifold assemblies to structural repair and bespoke fabrication.
Read moreWorn and damaged components restored to serviceable condition, typically at a fraction of the cost of buying new.
Read moreMost enquiries start with a description of a problem rather than a specification. Tell us what the machine is doing and we will work out the rest.
Get in touch